Feedwater Heating with Ejectors: Improving Deaerator Efficiency
Jetomat ejectors improve deaerator efficiency by capturing vented flash steam from condensate receivers and recompressing it for feedwater heating.
On this page
Introduction
Most boiler houses still vent flash steam from condensate receivers or relief points—hot vapour that could be preheating your feedwater. Every kilogram of low-pressure steam you keep on site is one you don’t have to generate again. A Jetomat controllable steam jet ejector (a thermocompressor) makes this easy: it pulls low-pressure vapour that would have been lost and recompresses it to a useful pressure for the deaerator (DA) or feedwater tank. The outcome is simple and measurable: energy saved, reduced boiler firing, fewer visible plumes, and better overall boiler efficiency.
What is ejector-driven feedwater heating?
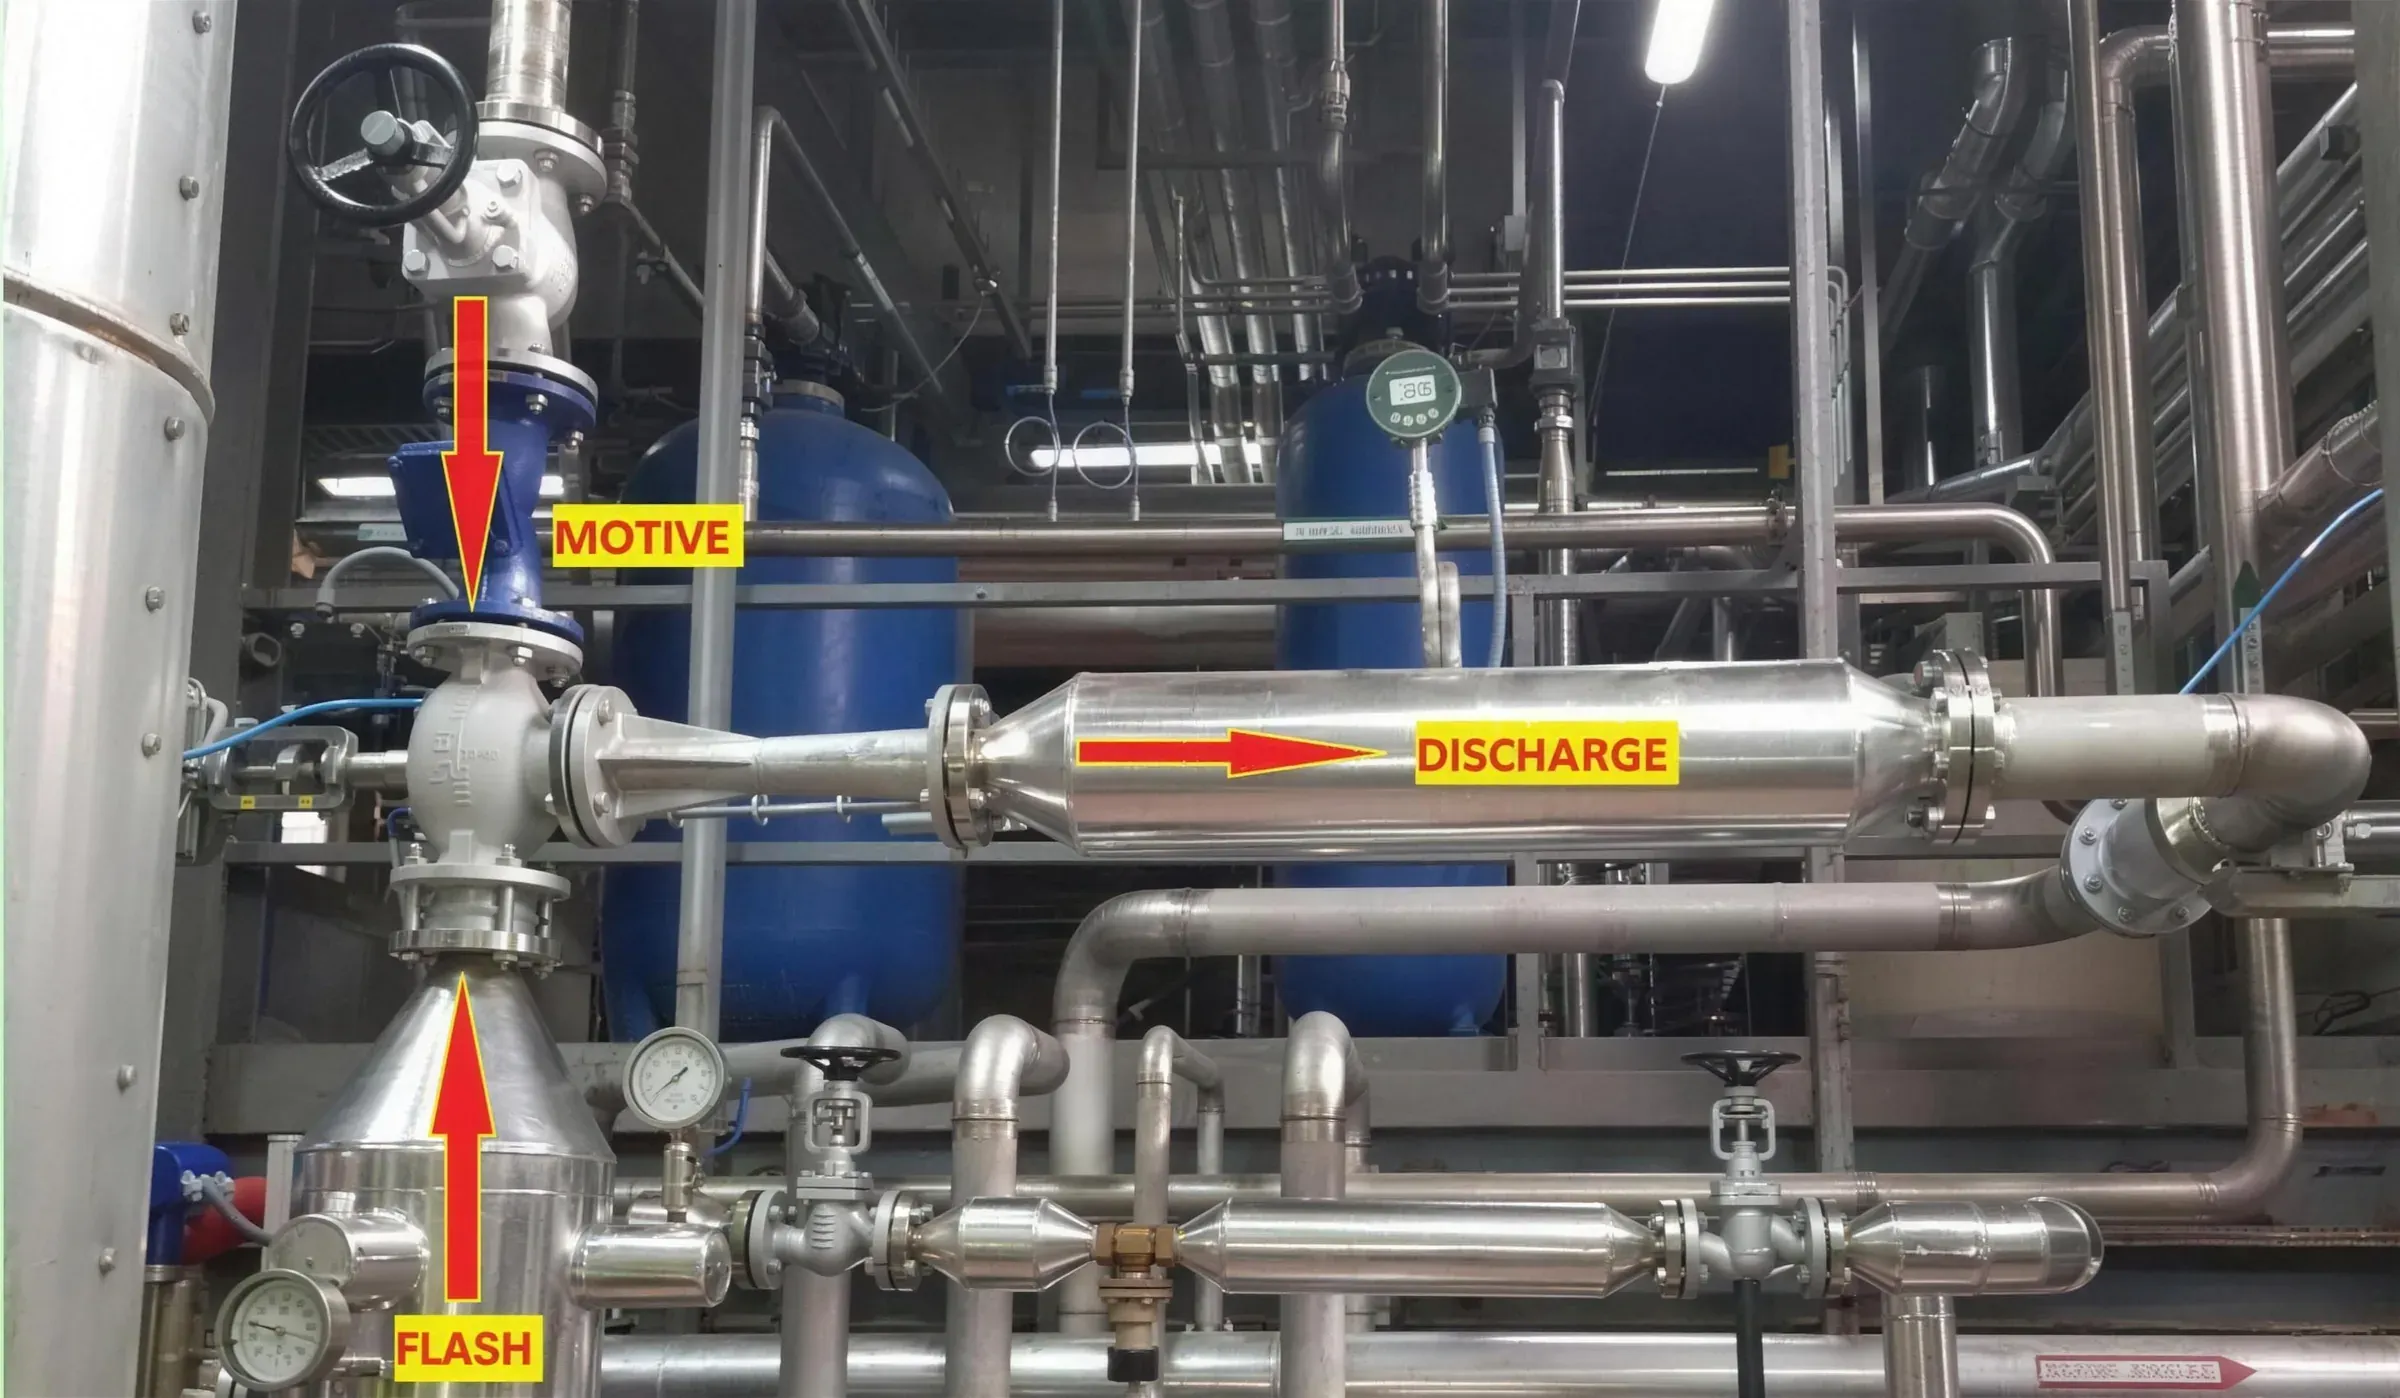
Ejector-driven feedwater heating uses a controllable Jetomat to entrain low-pressure vapour (vent/flash steam) and discharge mixed steam directly into the DA or feedwater tank—a clean form of heat recovery.
How it works:
The motive nozzle accelerates a small flow of high-pressure steam.
The high-velocity jet creates vacuum in the mixing chamber, entraining low-pressure vapour (the “waste”).
The diffuser converts velocity back to pressure so the mixed steam can heat your DA at the target pressure/temperature.
This is the classic steam jet ejector principle—a momentum-exchange steam compressor with no rotating machinery (only the nozzle spindle moves).
Components of the setup
Jetomat controllable nozzle (with spindle/actuator): Modulates motive flow; typical rangeability 3:1–5:1.
Suction take-off: From an atmospheric flash tank or open condensate receiver (typical suction: ~0 to 0.3 bar(g), 100–105 °C).
Mixing chamber + diffuser: Set the achievable entrainment ratio (ω = suction flow ÷ motive flow) and compression ratio (π = p4 ÷ p2).
Discharge target:
Atmospheric DA / feedwater tank: ~0 bar(g), 102–105 °C.
Pressurised DA: 0.2–0.3 MPa abs (~2–3 bar abs), 120–134 °C.
Minimal extras: A small steam separator downstream only if uber-dry steam is required at instruments; most DAs accept slightly wet saturated steam.
Controls & safety: Mixed-pressure PID to the motive valve; suction low-flow alarm; DA high-temperature/pressure interlocks integrated with the existing heating-system logic.
Why do it?
Lower boiler firing – Every kg/h of recovered vapour injected into the DA displaces ≈ 1 kg/h of fresh boiler steam for feedwater heating.
Reduced thermal pollution – The roof plume disappears; less vent noise; better neighbourhood relations.
Water & chemicals drop – Keeping steam and condensate in the loop trims make-up water and dosing.
Robust reliability – No rotating machinery; ejectors are maintenance-light.
Scales well – Works from small packaged plants to campus boilers; easy tie-in to LP headers if you want the mixed steam elsewhere.
How much steam (and money) can you save? - A quick energy balance
Goal: Route waste vapour into the DA to hit the DA temperature setpoint with less fresh steam.
A) Atmospheric DA example DA setpoint: 103 °C (~0 bar(g))
Suction source: Open receiver vent, 400 kg/h of flash steam at 100–102 °C
Motive header: 8 bar(g)
Jetomat sizing (indicative): Choose entrainment ratio ω ≈ 0.8, so motive ≈ 500 kg/h, mixed ≈ 900 kg/h to DA.
Displacement rule: 400 kg/h recovered → ~400 kg/h less fresh steam to the DA.
Annual energy value:
0.4 t/h × 8,000 h/y = 3,200 t/y
Multiply that by your all-in steam cost per tonne (fuel + water + chemicals) for the annual saving in Rs.
Numbers scale linearly: halve the recovered flow → half the savings; pressurised DAs typically show even higher value per ton due to higher saturation temperatures.
B) Pressurised DA example (higher value per kg)
DA pressure: 2.5 bar abs (≈1.5 bar(g)), 127 °C
Recovered vapour: 300 kg/h (from flash tank)
Each kg/h recovered offsets nearly one kg/h of DA heating steam at 127 °C, which is costlier per unit than at 103 °C—so the savings climb.
Control philosophy
Primary loop: Hold mixed pressure (or DA temperature) via the Jetomat’s controllable nozzle; typical steady-state pressure band ±0.05 bar and temperature ±0.5 K.
Load swings: With a modern actuator, response is typically < 2–5 s to DA pressure/temperature steps—ideal when condensate return fluctuates.
Integration: Standard 4–20 mA/fieldbus into PLC/DCS; alarms for low suction temperature/flow to avoid “pulling air” from an empty receiver.
Practical piping & instrumentation
Suction line: Short, insulated, large-radius bends; no low pockets (avoid slugging); include a strainer.
Discharge to DA: Enter above water line with proper dispersion; respect DA manufacturer’s recommendations.
Chemistry impact: Expect lower oxygen-scavenger consumption when DA temperature rises by 3–8 K from recovered vapour.
Turndown: Design for 3:1–5:1 motive turndown so nights/weekends (low vent) remain stable.
Optional polishing: If you must keep some local temperature control elsewhere, a small desuperheater can trim after the ejector.
Where the ejector fits in a boiler-house strategy
Deaerator “pre-heater”: The Jetomat acts as a thermal vapour recompressor, using a small motive flow to lift waste vapour into the DA—a net energy saving.
LP header support: If DA has enough heat, divert mixed steam to an LP header (2–3 bar) to serve auxiliary users (humidifiers, small coils).
Plant-wide fit: Combine with condensate return upgrades, trap surveys eliminated or reduced via ejector-based recovery, and roof-vent abatement—flash steam recovery becomes an integral part of the plant.
FAQ
Q1. Do I need a steam separator after the ejector?
A. Not for a DA. DAs like saturated (even slightly wet) steam; a separator is usually unnecessary. For instrumentation-sensitive users, add one.
Q2. Will it upset DA pressure control?
A. No—Jetomat’s discharge is pressure-controlled. It behaves like a smart steam source that tracks the DA’s setpoint.
What if the vent flow varies a lot?
A. The controllable nozzle tracks it. If suction falls, motive reduces; if suction surges, the ejector opens to keep the DA steady.
Conclusion
Ejector-driven feedwater heating is a fast, low-maintenance way to boost deaerator efficiency, cut boiler firing, and erase roof plumes. The physics are simple, the controls are straightforward, and the savings are real—every kg of vented steam you capture displaces about a kg of fresh boiler steam, with upside at higher steam costs or pressurised DAs.
How to proceed (4 steps):
Measure the vent: Log temperature/pressure and average kg/h from your flash tank or condensate receiver.
Define the sink: Atmospheric DA or pressurised DA; note setpoint pressure/temperature and available nozzles.
Get a sizing check: Ask for a thermocompressor design check (entrainment ratio, compression ratio, nozzle and diffuser geometry, turndown).
Pilot & prove: Trend boiler firing, DA temperature, make-up water, and chemical use for 2–4 weeks; validate the savings and roll out.
Where to go next