Topic · Thermocompressors: fixed vs variable
Controllable vs. Fixed Ejectors: Why Modulation Matters
Fixed ejectors work well at only one design point. A controllable Jetomat modulates with load, avoiding lost suction and wasted steam.
- Author
- Nitant Harani
- Published
- Reading time
- 5 min read
INTRODUCTION
Paper machines don’t run at one perfect point all day. Basis weight changes, sheet speeds change, seasons change—and your headers move with them. A traditional fixed-nozzle steam ejector (a fixed thermocompressor) is tuned for a single design point; off that point it can lose suction or over-compress, forcing bypasses and wasting steam. A Jetomat controllable ejector solves this with a variable-area motive nozzle driven by an actuator: it trims the jet to the actual load so mixed pressure stays put and suction holds—even as conditions swing. Think of it as a globe valve vs. a control valve: fixed nozzle ≈ globe (one position), variable nozzle ≈ a true control valve.
WHAT IS A CONTROLLABLE VS. A FIXED EJECTOR?
Fixed-nozzle ejector
Single geometry: nozzle → mixing chamber → diffuser.
Narrow control window: one design point, and it drifts off set-point as load moves.
Works best at constant demand; needs a higher motive pressure to stay on map.
Controllable Jetomat ejector
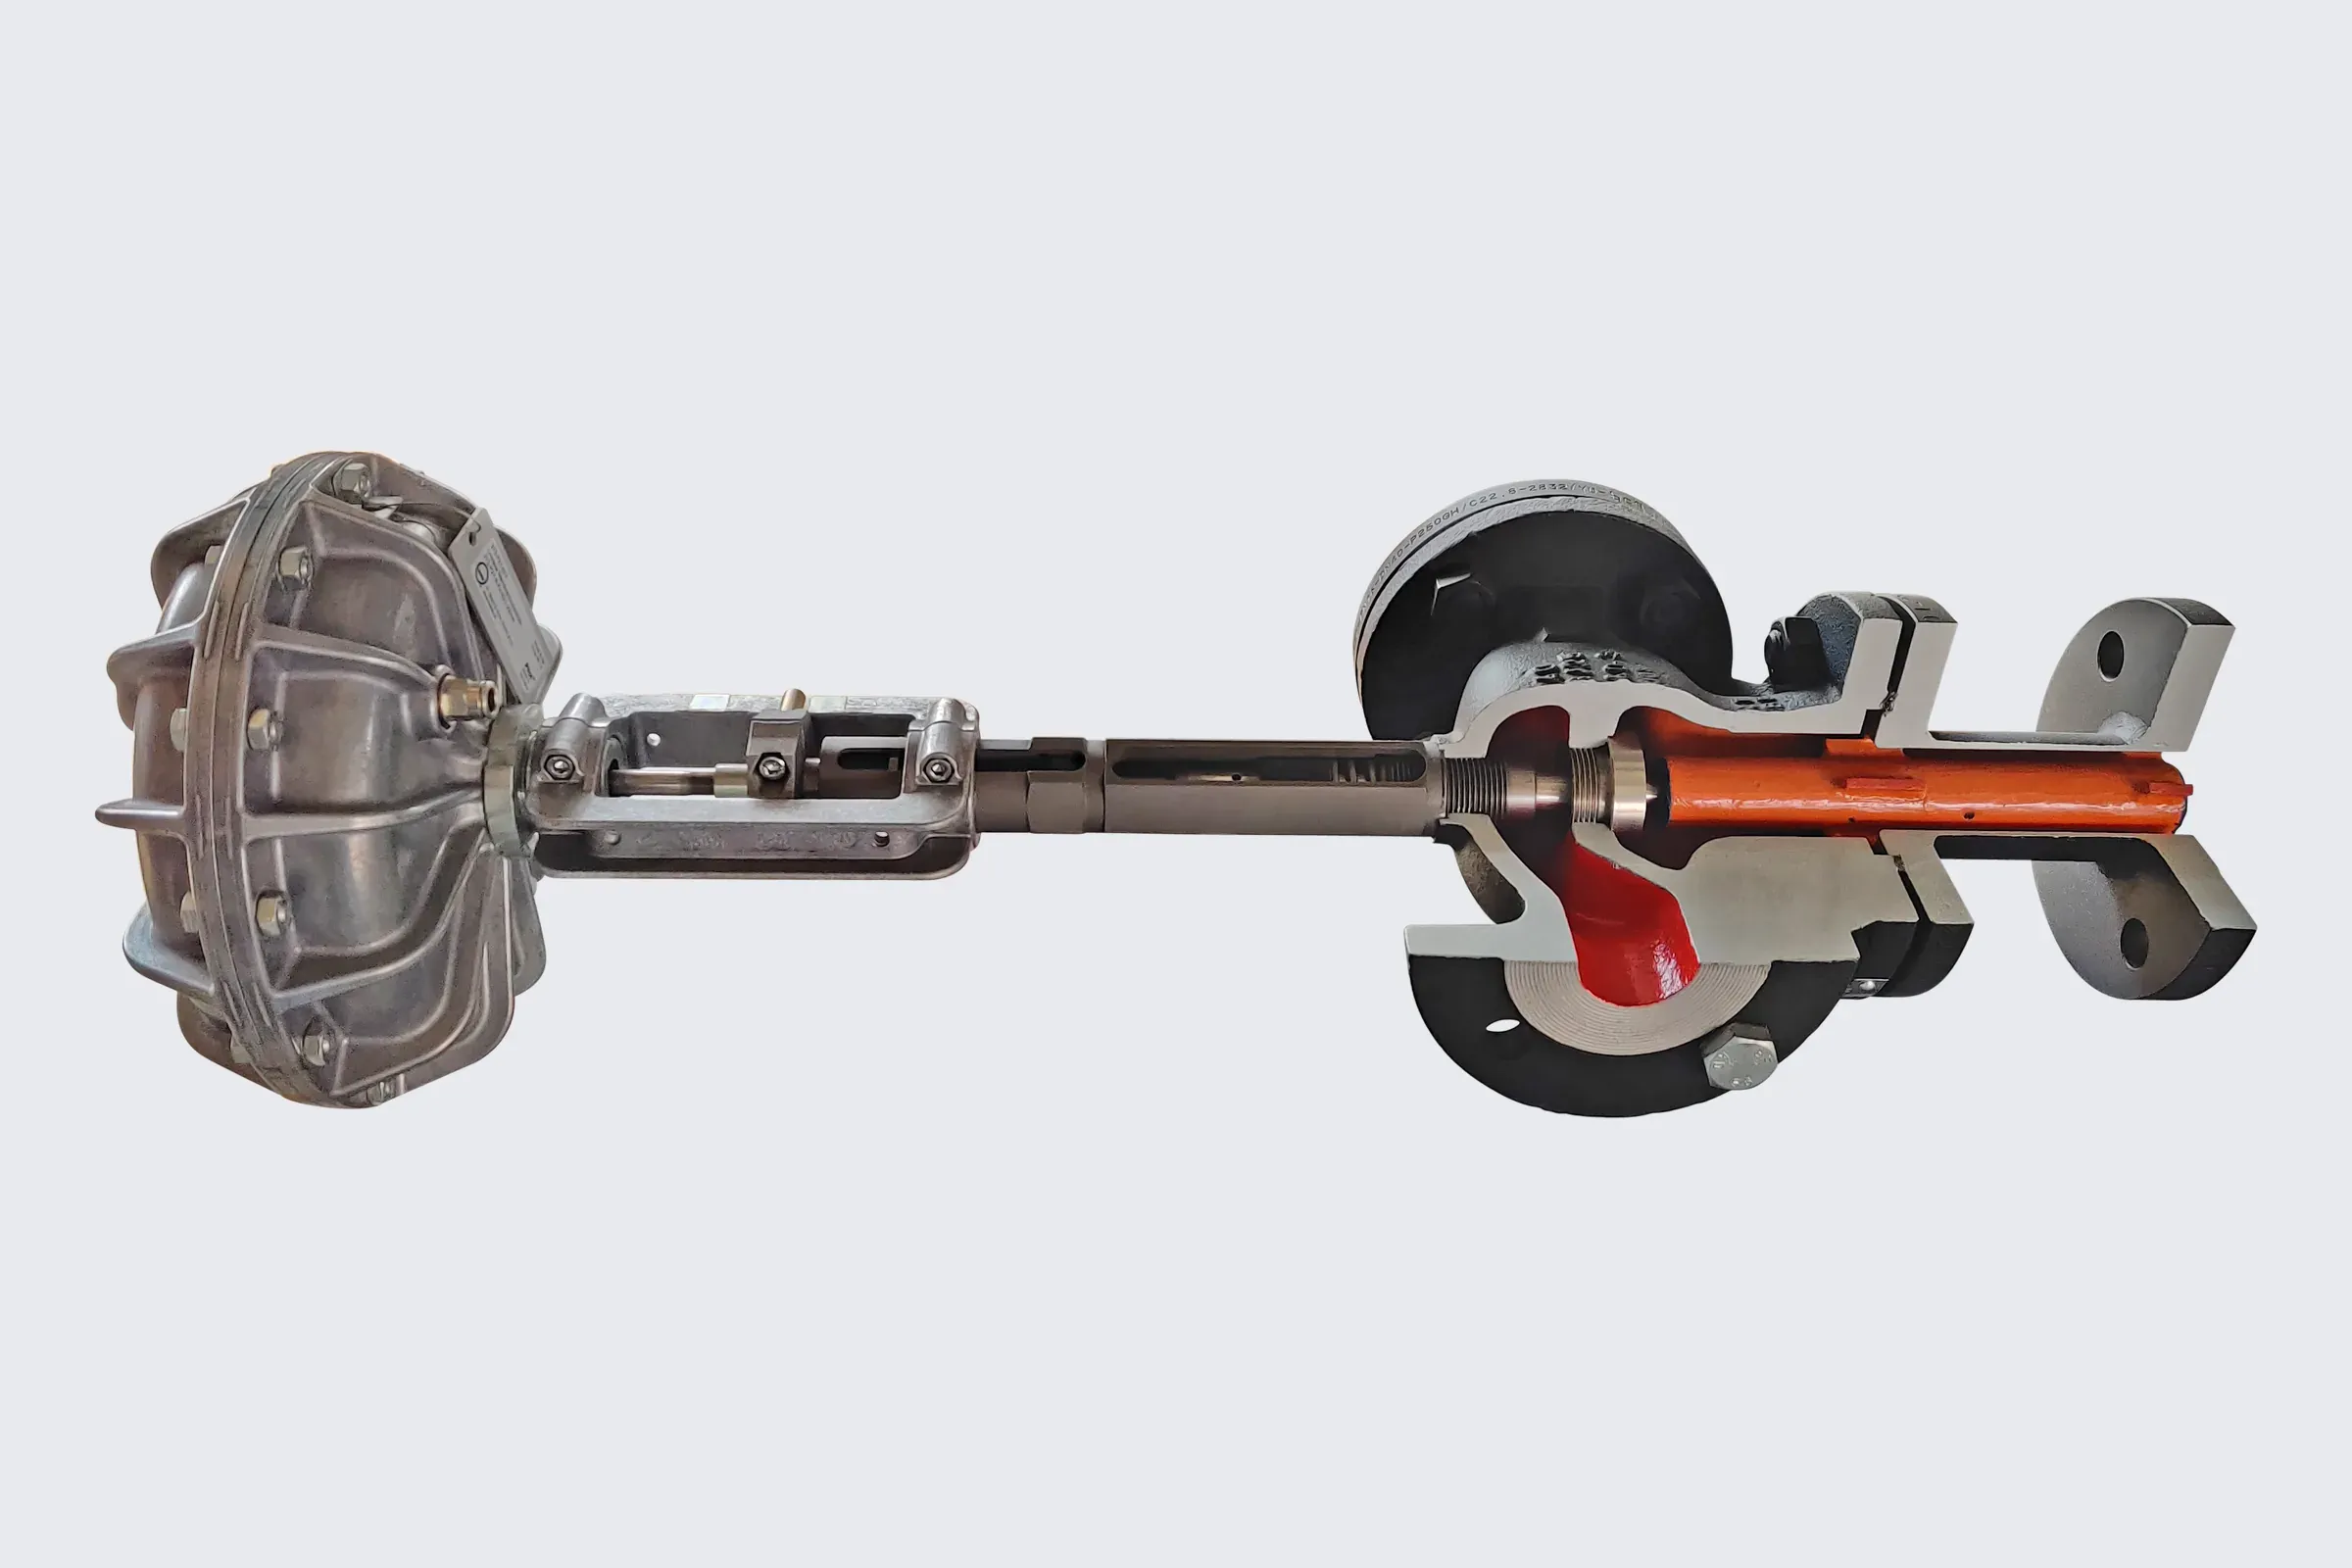
Same hydrodynamics, but the nozzle throat area (At) is modulated via a spindle and actuator (pneumatic or electric).
Wide effective range; control from ~10–15% up to 70–80% of capacity is typical.
Holds discharge/mixed pressure constant under changing motive or suction conditions, and can operate even with low motive pressure (1–3 barg) in many services.
Core physics: Venturi/Bernoulli. Accelerating the motive jet drops static pressure (vacuum) to entrain suction vapour; the diffuser reconverts velocity to pressure—the classic steam jet ejector principle for compressible media.
COMPONENTS
Variable-area motive nozzle
Actuator + positioner move the spindle to change At, thereby tuning motive mass flow, jet Mach number and entrainment.
Pneumatic (fast, spring fail-safe) or electric (fieldbus-friendly) options.
Mixing chamber
The high-velocity jet entrains low-pressure vapour (flash steam) from returns/dryers; momentum exchange happens here.
Diffuser
The diffuser and nozzle pairing sets feasible compression and turndown; pressure is recovered to your setpoint.
Controls
PID on mixed-steam pressure (or temperature proxy) drives the actuator; stability across the operating map is the whole point of modulation.
These parts are custom-sized per application to cover your min/normal/max conditions rather than a single point.
WHY MODULATION MATTERS
Two non-negotiables describe ejector behaviour:
Entrainment ratio (ω = suction flow ÷ motive flow) (suction/motive)
Compression ratio (π = mixed pressure ÷ suction pressure)
A fixed nozzle locks you to one (ω, π) operating point. When header pressure drops or suction rises, you slide off the map → loss of suction or over-compression.
A variable nozzle shifts At to re-centre operation—keeping suction and mixed pressure stable across 10–15% up to 70–80% load range (vs. one design point for fixed). That’s why controllable units fit fluctuating demand or fluctuating boiler supply, not just steady duty.
PAPER-MACHINE EXAMPLES
A) Day–night production swings on a dryer group
Target mixed pressure: 3.5 barg; Motive header: 9–11 barg across the day.
Suction (flash) flow: 1.0–2.2 t/h as sheet speed/GSM changes.
Fixed-nozzle: sized for 1.6 t/h.
At 1.0 t/h, the device over-compresses; you see hot spots, controller fights, vents crack.
At 2.2 t/h, suction collapses; traps lift, moisture profile drifts.
Controllable Jetomat:
Closes the nozzle at low load to avoid over-compression; opens at high load to preserve entrainment.
Mixed pressure holds within a tight band; sheet temperature variation shrinks, enabling speed increases and fewer breaks. (The steam saving vs. throttling is up to 30%, Baelz: 10–30% in compression, when recovery stays engaged off-design.)
B) Seasonal header variation (winter 11 barg, summer 9 barg)
A fixed nozzle needs motive margin above its design point; in summer afternoons suction can fall out.
A controllable unit opens the nozzle at lower motive pressure to hold setpoint, so flash steam recovery keeps running—no afternoon plumes, no PRV work-arounds.
SIDE-BY-SIDE: FIXED VS. CONTROLLABLE
| Attribute | Fixed nozzle | Controllable (Jetomat) |
|---|---|---|
| Usable control range | One design point; drifts off set-point as load moves | ~10–15% to 70–80% of capacity |
| Motive pressure need | Set by its one design point | Can work from 1–3 bar(g) (service-dependent) |
| Discharge pressure at varying loads | Drifts off setpoint | Holds constant vs. motive/suction swings |
| Energy use of motive | Off the design point, part of the motive is throttled | ~100% used for recompression (no separate throttling) |
| Best for | Fixed load applications | Dynamic demand/boiler variability |
| Typical steam savings | Baseline at design point | Up to 30% (Baelz: 10–30% in compression) |
BENEFITS
Energy & steam economy
Holding suction through swings keeps the ejector in compression mode (not bypass), so you genuinely reuse flash steam instead of venting it. Plants targeting dynamic operation see double-digit energy savings, year after year.
Quality & throughput
Stable mixed pressure → thinner condensate films on cans → stronger heat transfer and flatter temperature profiles. That improves moisture control and reduces warp/wrinkles on lightweight grades.
Reliability
Variable-nozzle units avoid the off-design “dead zones” where fixed units chatter or lose suction. Baelz notes many replacements of failed fixed thermocompressors with the variable-area design for this reason.
Lifecycle cost
While a controllable unit includes actuator/positioner, the slides show the 10-year operating cost is lower because fuel/steam savings dominate—especially where demand varies.
PRACTICAL SELECTION
Is energy efficiency a priority (steam cost high)? If yes → favour controllable.
Is demand or suction pressure variable? If yes → variable nozzle; if truly constant → fixed can suffice.
Required turndown? If >10–20%, choose variable; fixed is comfortable only close to its design point.
Bonus: You can pair the controllable nozzle with either pneumatic actuation (fast, spring fail-safe) or electric (digital integration)—pick based on loop speed, environment, and utilities. (See our actuator guide for details.)
IN SHORT
A Jetomat’s variable nozzle and diffuser keep steam and condensate in circuit: the unit works as a compact steam compressor, turning flash steam into useful mixed steam for your heating loads. Plants often run fewer traps as a result, and rarely need a separate steam separator at the user.
CONCLUSION
Fixed ejectors are fine at one point; modern paper mills need performance across many points. A controllable Jetomat tracks your process—basis weight changes, header dips, seasonal swings—so suction and mixed pressure remain on spec, energy is reused (not vented), and runnability improves.
What to do now
Map min/nominal/max for motive pressure, suction flow/pressure, and target mixed pressure on each dryer group.
Flag where fixed units are bypassed or unstable (loss of suction, over-compression).
Request a thermocompressor design check (entrainment map sized to 10–15% → 70–80% control range; motive as low as 1–3 barg if applicable).
Pilot a controllable unit; track mixed-pressure stability (±0.05 bar), steam/ton, and moisture profile over 2–4 weeks.
Standardise across groups to lock in steam savings of up to 30% (Baelz: 10–30% in compression) where variability is high.
The physics behind this, nozzle, entrainment ratio, fixed versus variable, is free in the i-Kcal Thermal Academy: Thermocompressors: fixed vs variable.
See the product: Jetomat Thermocompressor. See it in your industry: Paper & Tissue.