Stop Venting Steam: A Textile Mill Recycles Waste Steam with Thermocompressors
A textile mill vented its dryer flash steam. A Jetomat thermocompressor now recompresses it into the drum supply: less boiler fuel, fewer traps, steadier drying.
On this page
- The problem: visible vent = visible loss
- The fix: install a thermocompressor on the vent
- Simple science: how the ejector works
- The key number: 1 kg in = 1 kg avoided
- What changed on the ground
- Tangible plant-level results
- Hidden win: better heat transfer & fabric quality
- Fewer traps, simpler loop
- Practical integration tips
- Why not just use a PRV?
- Next Steps
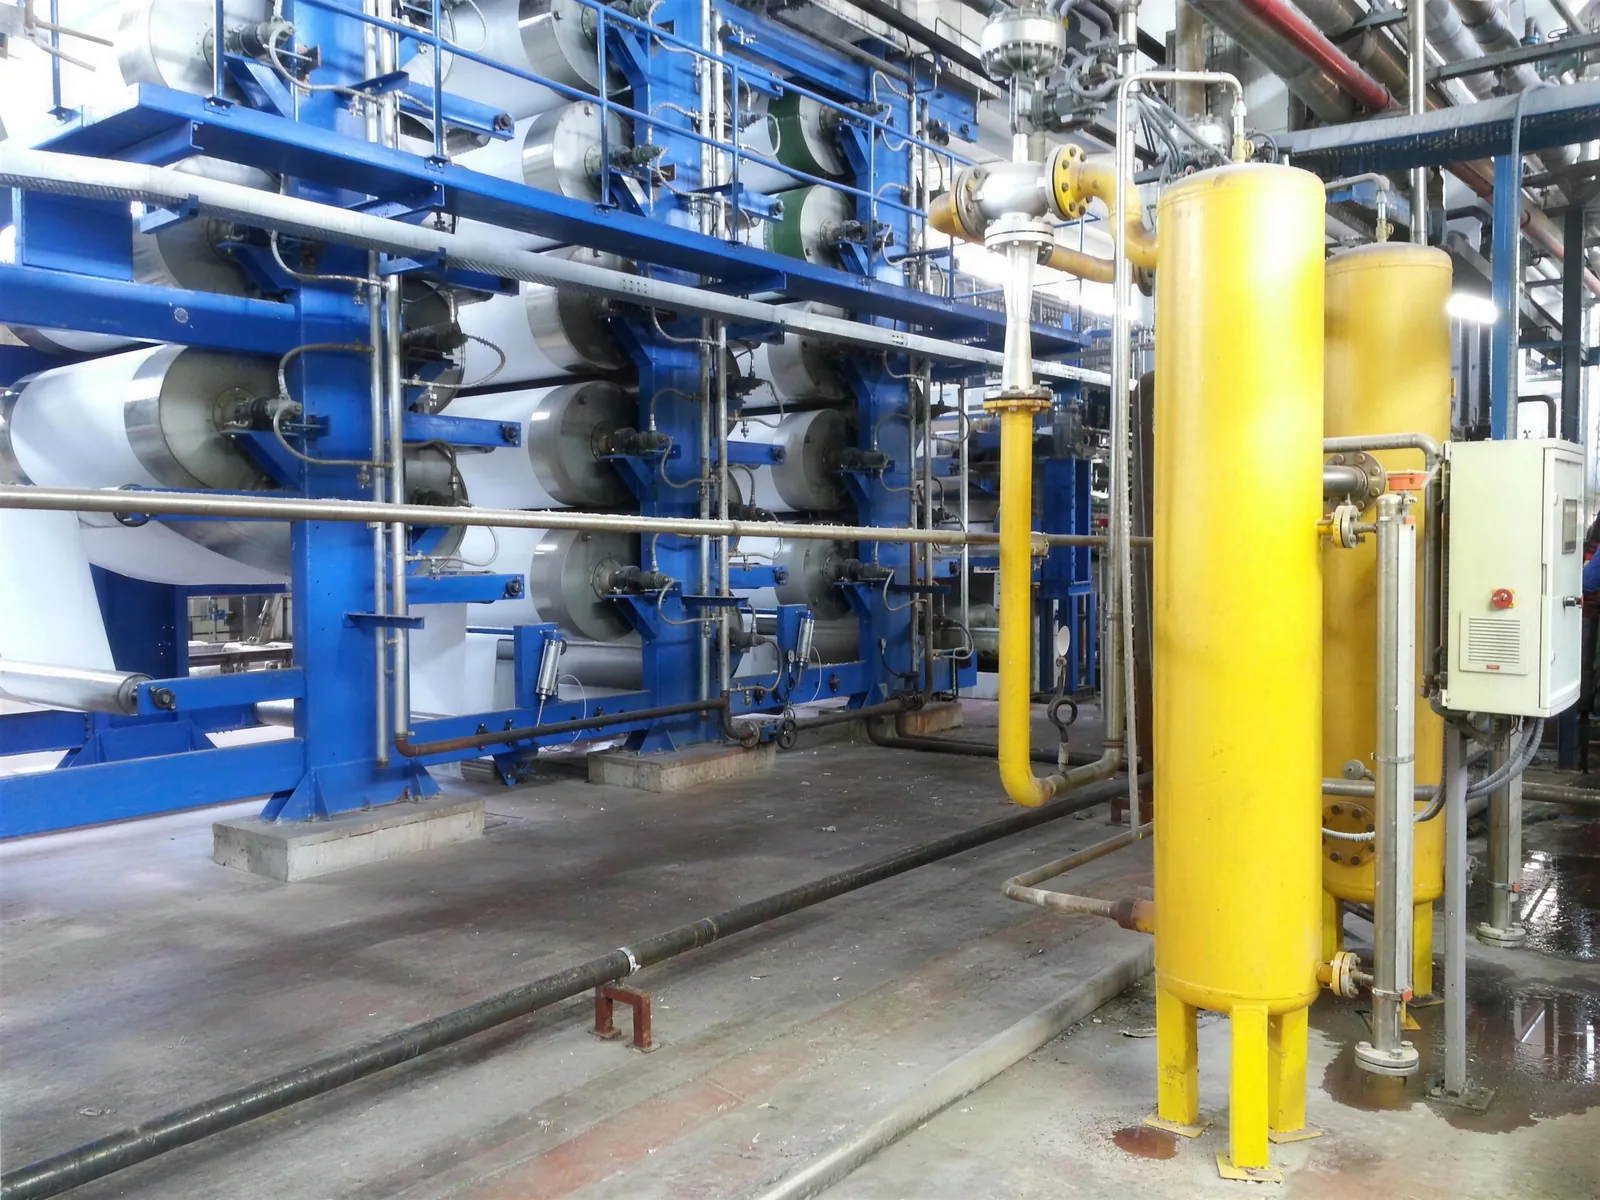
Textile industry
Introduction
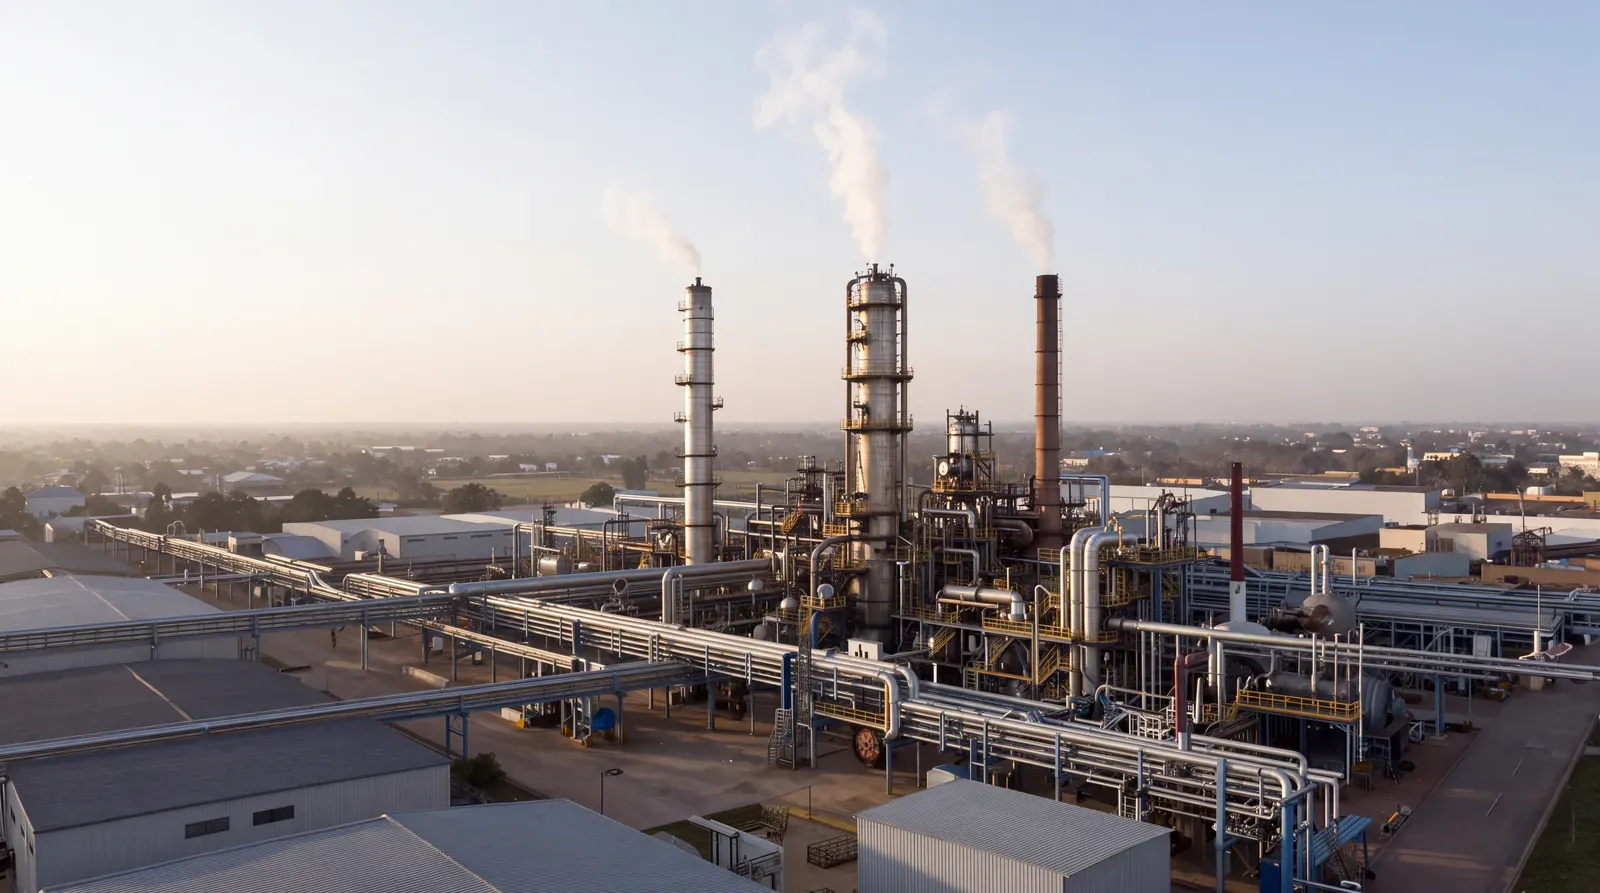
Many textile mills still vent low-pressure exhaust to atmosphere—those big white “steam clouds.” That’s avoidable energy loss. A steam thermocompressor captures that flash steam & recompresses it back into the process. Below is a practical, numbers-first walkthrough of how one textile plant eliminated visible venting, cut boiler fuel, & simplified its steam & condensate loop.
The problem: visible vent = visible loss
Vented flash steam is fuel you already paid for, escaping your site. In a typical textile plant, low-pressure (<2 bar) exhaust from washers/dryers was released directly to atmosphere—pure waste that also disturbed pressure balance & humidity around the line.
A Baelz textile note calls this “an avoidable waste of energy,” confirming many plants vent low-pressure steam unnecessarily.
The fix: install a thermocompressor on the vent
Instead of dumping 2 bar vapour, the mill fitted a thermocompressor to draw in that vapour & compress it using motive steam from the high-pressure main (about 10 bar(g)); at this gentle lift roughly 1.1 kg of motive moves 1 kg of vapour (a Baelz selection gives ω ≈ 0.9). The device then regulates the mixed steam back to the consumer setpoint (3 bar), turning a vent into recovered heat for the process.
Result: the plant no longer emits direct exhaust steam.
Simple science: how the ejector works
High-pressure motive steam accelerates through the variable nozzle.
That jet creates suction, entraining the low-pressure flash steam from the vent.
In the diffuser, velocity is turned back into pressure—delivering usable mixed steam at ~3 barg.
That’s the whole principle: a compact vapour compressor with no rotating machinery.
The key number: 1 kg in = 1 kg avoided
Every kilogram of 2 bar steam recovered by the jet pump reduces the demand for 3 bar steam by 1 kg. That 1:1 displacement is why thermocompression saves energy so directly—you immediately cut fresh boiler steam.
What changed on the ground
Before: 3 barg consumers ran entirely from fresh boiler steam.
After: a Jetomat mixes 10 barg motive steam with 2 barg suction & controls the mixture to 3 barg—so consumers see the same pressure, but the boiler now supplies much less fresh steam overall.
Tangible plant-level results
No more steam clouds: “The entire plant no longer emits direct exhaust steam.”
Lower fuel: every recovered kg reduces firing. In similar textile dryer retrofits (valves → ejectors), mills saw ≈15% steam savings (1-row line) & ≈20% on larger, 3-row lines—plus trap removals.
Water & chemicals down: keeping condensate/flash in-loop lowers make-up water & treatment demand (documented strongly in paper/corrugated; principle holds in textiles).
Hidden win: better heat transfer & fabric quality
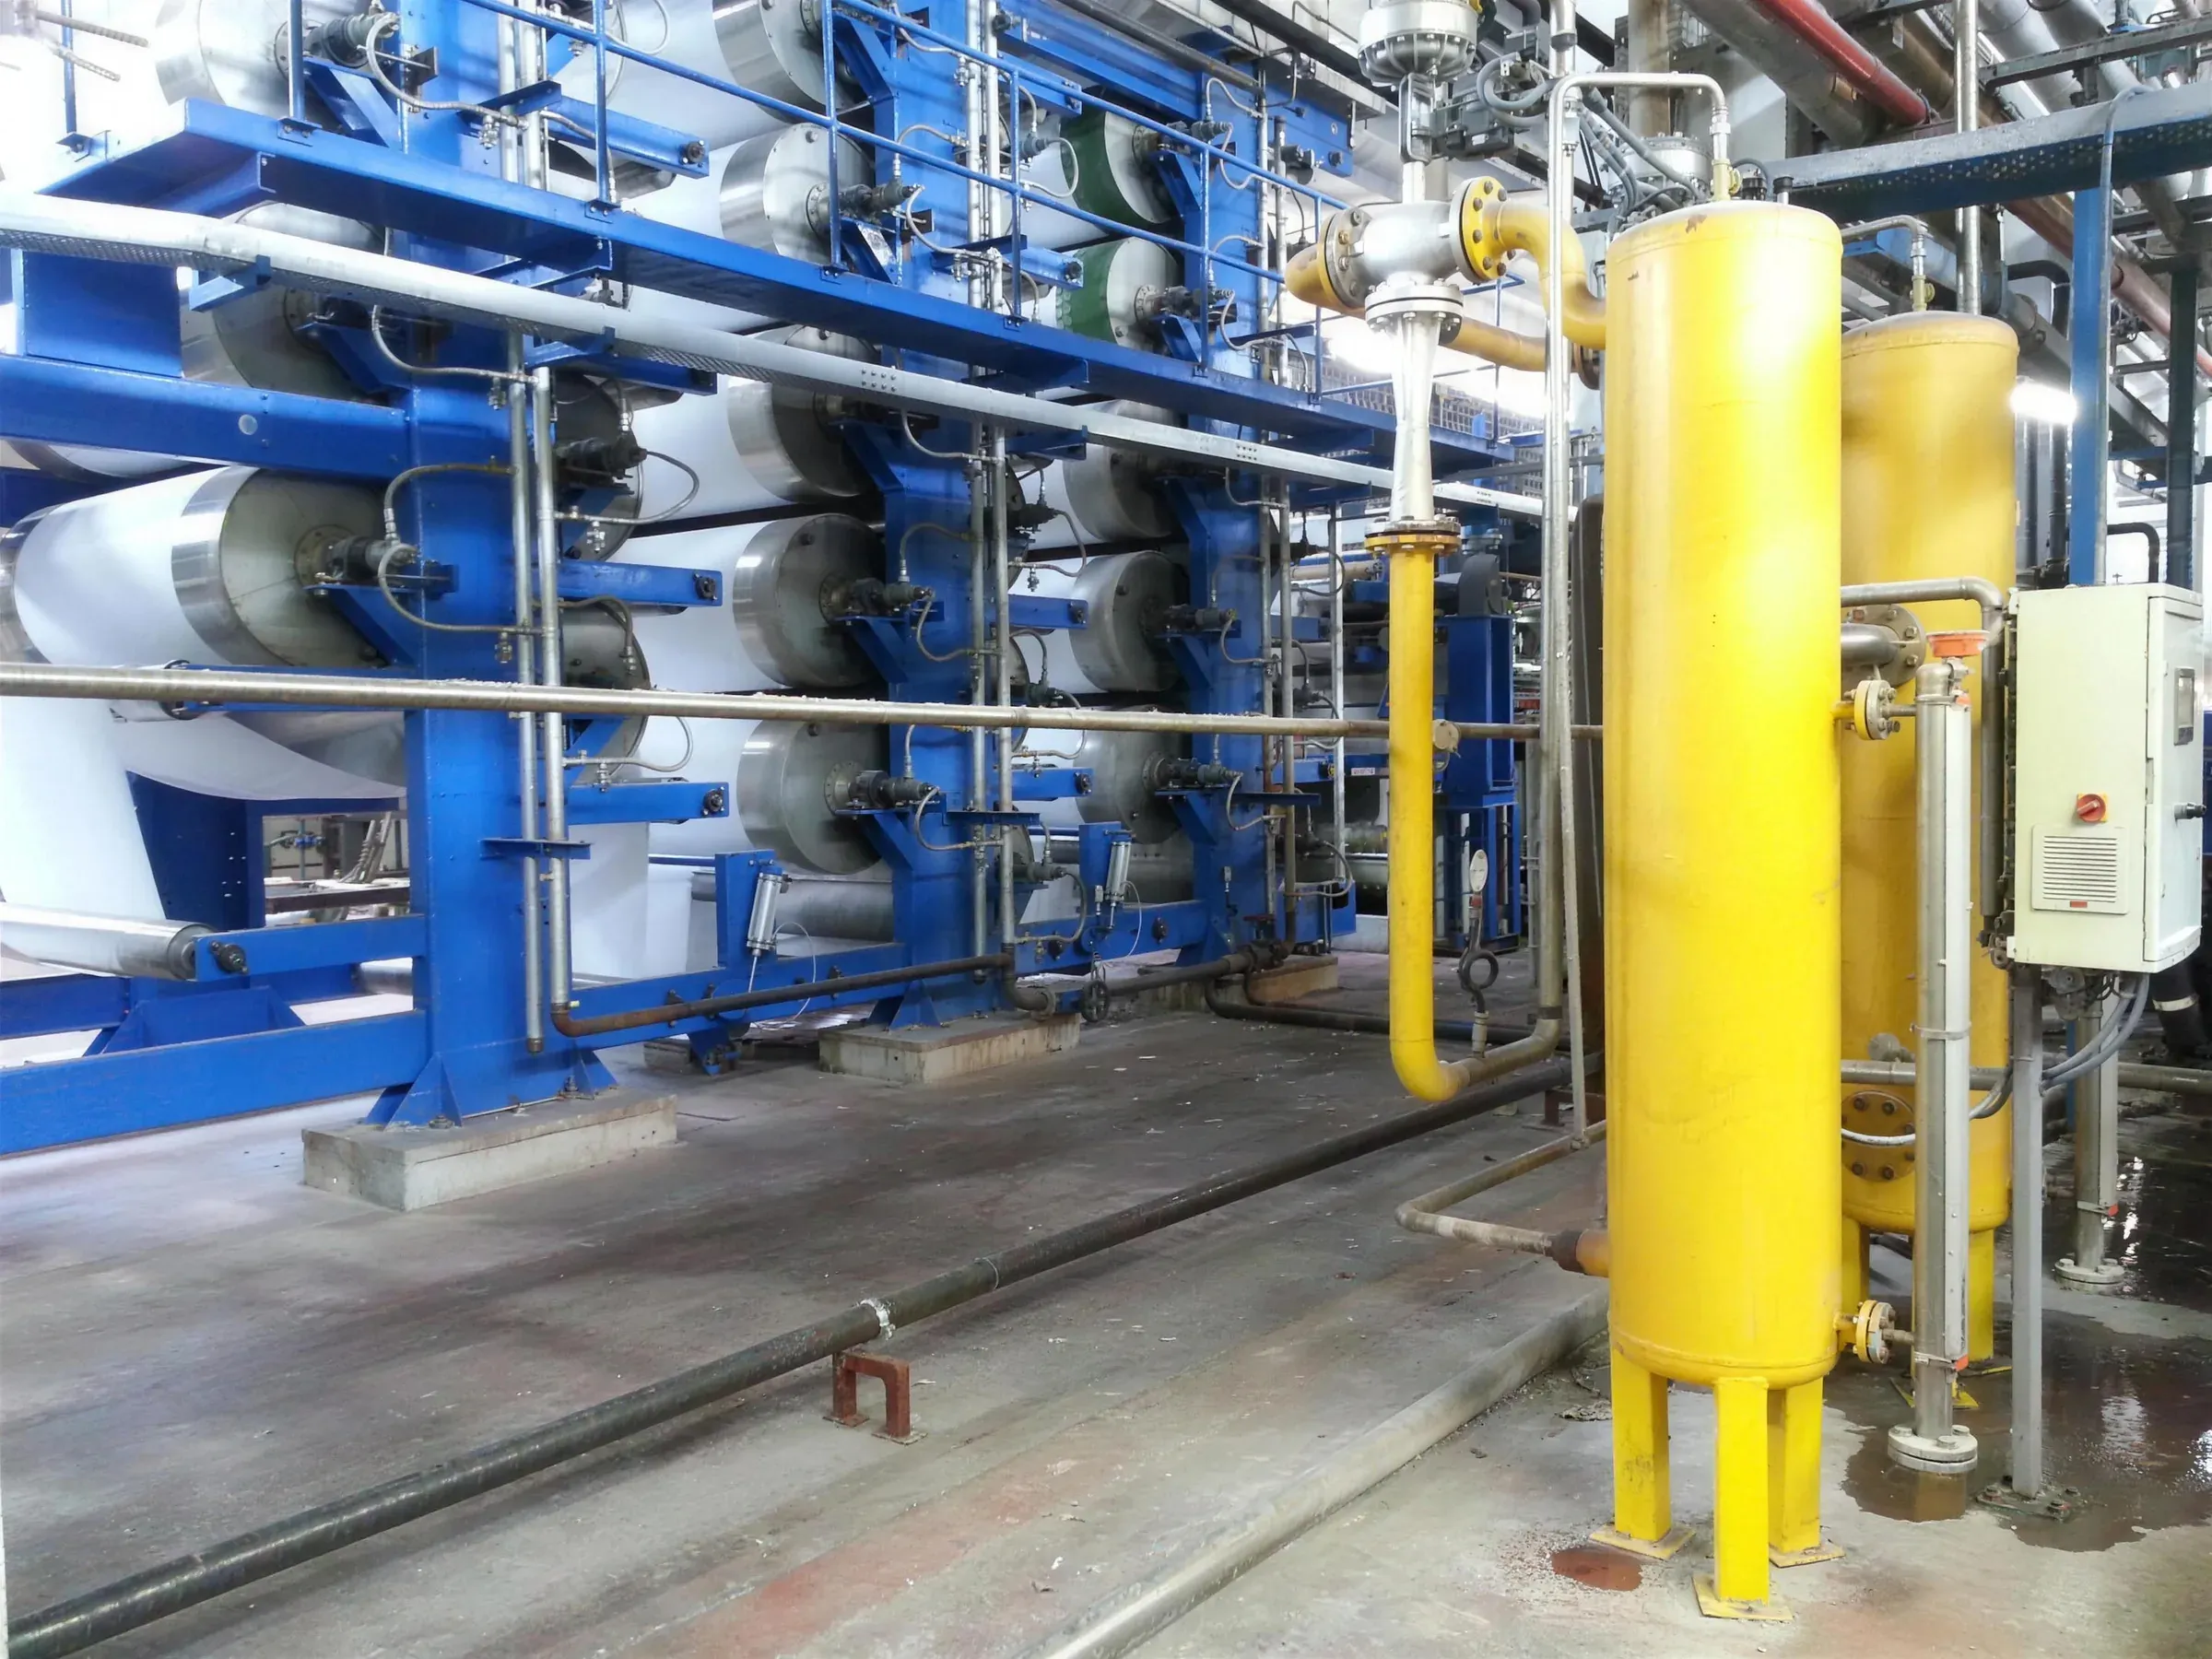
Higher internal steam velocity thins the condensate film on cylinders, improving heat transfer (hotter, more uniform drum surface for the same header pressure). Plants consistently report more uniform drying & the ability to nudge line speed upward after switching to ejectors.
Fewer traps, simpler loop
A thermocompressor continuously entrains flash vapour back into the loop. In many dryer sections, drum-level steam traps were removed or drastically reduced after installing ejectors—cutting maintenance & leak points. (A textile 1-row case eliminated post-drum traps entirely.)
Practical integration tips
Thermocompressor design: match motive/suction/mixed pressures & the expected vent rate; size for daily extremes.
Controls: regulate mixed pressure or downstream temperature with the Jetomat’s own variable nozzle: its actuated spindle sets the motive flow, so no separate control valve is needed on the motive line.
Piping: keep suction run short, avoid sharp restrictions; provide proper drainage. Often you can simplify or avoid a separate steam separator because flash recovery is now built into the loop.
Why not just use a PRV?
A PRV throttles—it doesn’t recycle. The exergy lost in throttling is gone, & you still vent flash elsewhere. A thermocompressor (Jetomat) converts that vent to useful mixed steam. That’s the difference between dropping pressure & re-using it. (In other sectors, right-sized ejectors have paid back in ~1.7 months; textiles with strong vent sources can see similarly fast returns.)
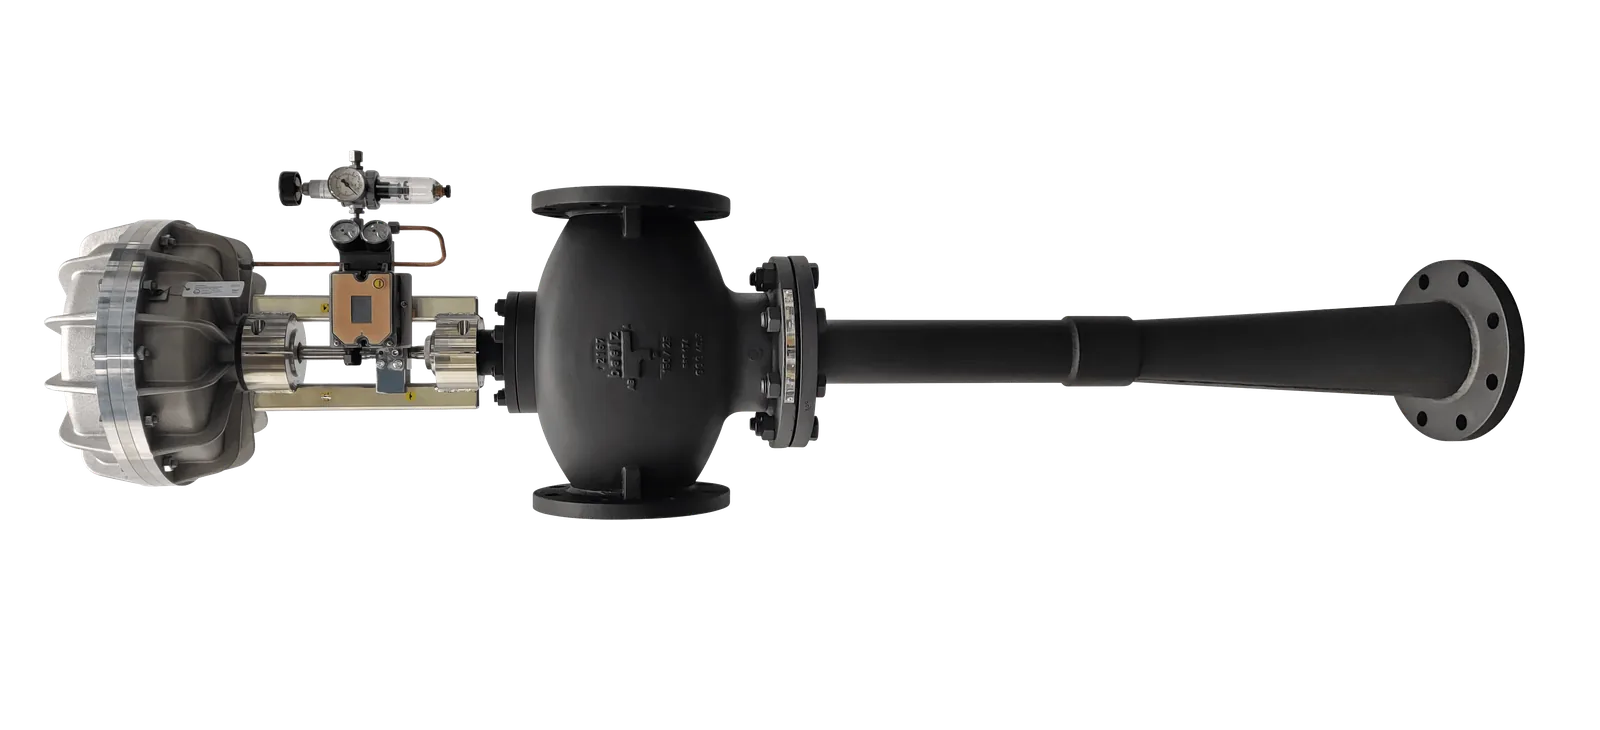
Jetomat (thermocompressor)
Conclusion
Thermocompression turns an atmospheric vent into controlled heat recovery. In this textile mill, a Jetomat captured low-pressure exhaust, stopped the steam clouds, & cut boiler fuel—while improving heat transfer & simplifying the steam & condensate loop. Start where the plume is biggest: measure the vent, size the ejector, pipe a short suction, & regulate mixed pressure. From there, scale across washers, dryers, & other users.
Next Steps
Walk through the line; identify the biggest vent.
Log pressures/flows; build a quick mass/energy balance.
Fit a pilot thermocompressor, verify the 1:1 kg displacement & fuel drop.
Roll out to remaining vents for cumulative energy savings across the plant.